
Choosing the Right Water Treatment for a Multi-Issue Well in Your Bakery

Pricing: request a quote
Get a Quote450,000 Grain Mineral-Tank Commercial Water Softener
✓ Free shipping in the USA · ✓ 90-day returns · ✓ Secure checkout
Understanding Your Treatment Choice Amidst Multiple Well Water Issues
Running a bakery means your water supply must support consistent operation and high-quality output. When your water comes from a well presenting several problems simultaneously—such as hardness, mineral buildup, and potential contaminants—the decision about which treatment approach to adopt becomes critical. It’s not just about improving water taste or clarity; it’s about safeguarding your equipment warranty, maintaining compliance with operational standards, minimizing staff downtime, and preventing costly disruptions to your trading hours.
As owner, operator, or facilities manager, you face the complex task of choosing a treatment method that addresses all these needs effectively. This page guides you through the classes of treatment available, the mechanisms by which they operate, why some may fall short in your specific situation, and what the right solution must deliver to ensure your bakery’s successful operations.
Exploring Treatment Classes and Their Operating Mechanisms
Various classes of water treatment exist, each with distinct methods for dealing with the challenges found in well water. The main classes to consider include:
- Filtration Systems: Utilizing physical screens or media to trap particles and suspended solids, improving water clarity but generally not addressing mineral hardness.
- Chemical Treatment: Involving the addition of chemicals to neutralize or precipitate undesirable components. Often complex to manage in high-demand commercial settings and requiring ongoing chemical supply and handling.
- Reverse Osmosis (RO): Employing semi-permeable membranes to remove a broad spectrum of dissolved solids and minerals. While thorough, RO systems tend to process water slowly and can generate significant wastewater, challenging for continuous high-volume needs.
- Water Softeners: Designed to exchange hardness-causing minerals like calcium and magnesium with sodium or potassium ions, effectively reducing scale formation and mitigating hardness-related issues.
Eliminating Unsuitable Treatment Approaches for Your Bakery’s Well Water
Given the specific needs of a bakery sourcing well water with multiple quality concerns, it is vital to reject treatment classes that fail to fully meet operational demands or impose unacceptable trade-offs:
- Filtration Systems: While useful for removing particulates, these do not address mineral hardness, which leads to scale buildup damaging baking equipment and reducing efficiency. They cannot be the standalone solution for your ‘total well’ problem.
- Chemical Treatment: The necessity to handle chemicals safely and the variability in water demand makes this impractical. It also risks inconsistent dosing, which could affect product quality and equipment integrity.
- Reverse Osmosis: Though effective at removing a broad range of dissolved substances, RO systems generally have slower throughput and higher maintenance. Their wastewater production is a major disadvantage for a high-demand bakery, risking service interruptions and increased operational costs.
This elimination narrows the field to water softeners, the class designed to specifically mitigate hardness and related mineral challenges without significant service disruption or complex handling requirements.
Criteria for a Suitable Water Softener in a Commercial Bakery Setting
The surviving treatment class—water softening—must meet stringent demands in this high-volume commercial environment:
- Capacity to Match High Water Demand: Your bakery needs a solution capable of continuous supply throughout operating hours, managing volume between 300,000 and 600,000 gallons without bottlenecks.
- Effective Mineral Removal to Protect Equipment: The softener must efficiently reduce hardness to prevent scale accumulation that can degrade ovens, boilers, and mixing hardware.
- Operational Reliability and Minimal Downtime: Equipment should support uninterrupted baking schedules, minimizing labor costs and avoiding lost production.
- Compliance and Warranty Preservation: Treatment must align with industry standards for water quality, ensuring your equipment warranties remain valid, and health regulations are met.
- Ease of Configuration and Maintenance: Units that ship ready to configure allow straightforward setup without dependency on external trades, facilitating smooth operation from day one.
The Documented Solution: A Commercial Water Softener from Nelsen Corporation
Meeting these requirements is the Nelsen 450,000 Grain Mineral-Tank Commercial Water Softener by Nelsen Corporation. Engineered specifically for high-demand commercial settings like bakeries, this softener manages substantial mineral loads with an effective grain capacity of 450,000. Its design supports ongoing operation aligned with your bakery’s trading hours, minimizing downtime and labor intervention.
By targeting hardness minerals, it protects your equipment from scale-related wear and preserves your operational reliability. The system ships ready to configure, providing you control and flexibility to accommodate your specific plumbing and space arrangements.
Choosing this approach ensures that your full spectrum of well water challenges is comprehensively addressed with a focus on service continuity, product quality, and compliance—critical factors in a busy commercial bakery environment.
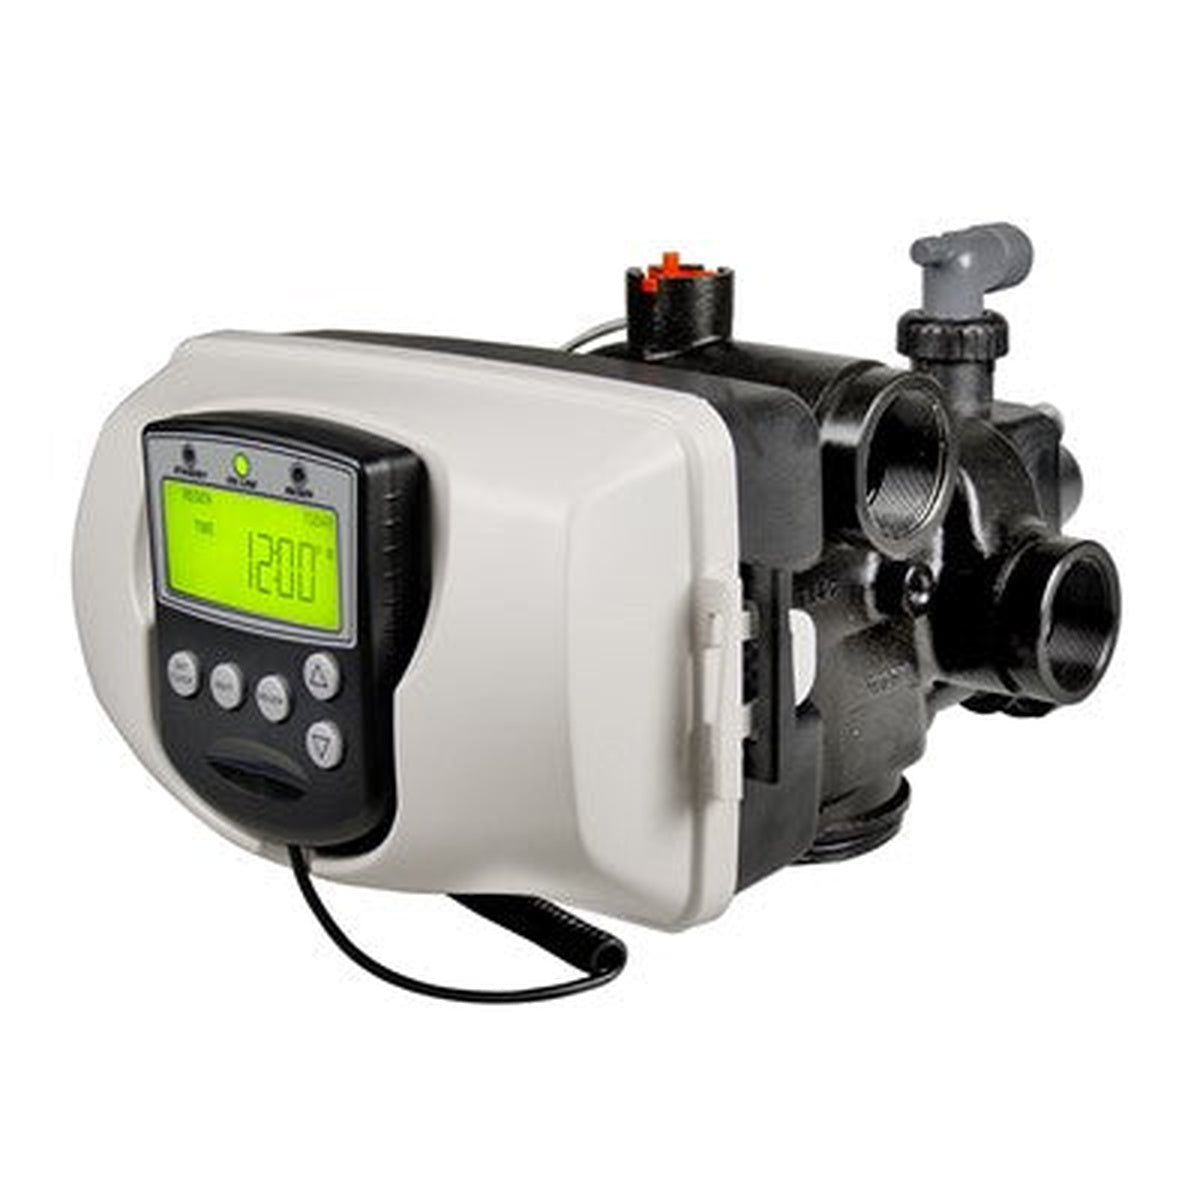
Nelsen 450,000 Grain Mineral-Tank Commercial Water Softener
Priced on request for your specification.