
Commercial Industrial Reverse Osmosis Usa Made 68825

Pricing: request a quote
Get a QuoteWater Softener Plus Industrial Reverse Osmosis System — 4800 GPD
✓ Free shipping in the USA · ✓ 90-day returns · ✓ Secure checkout
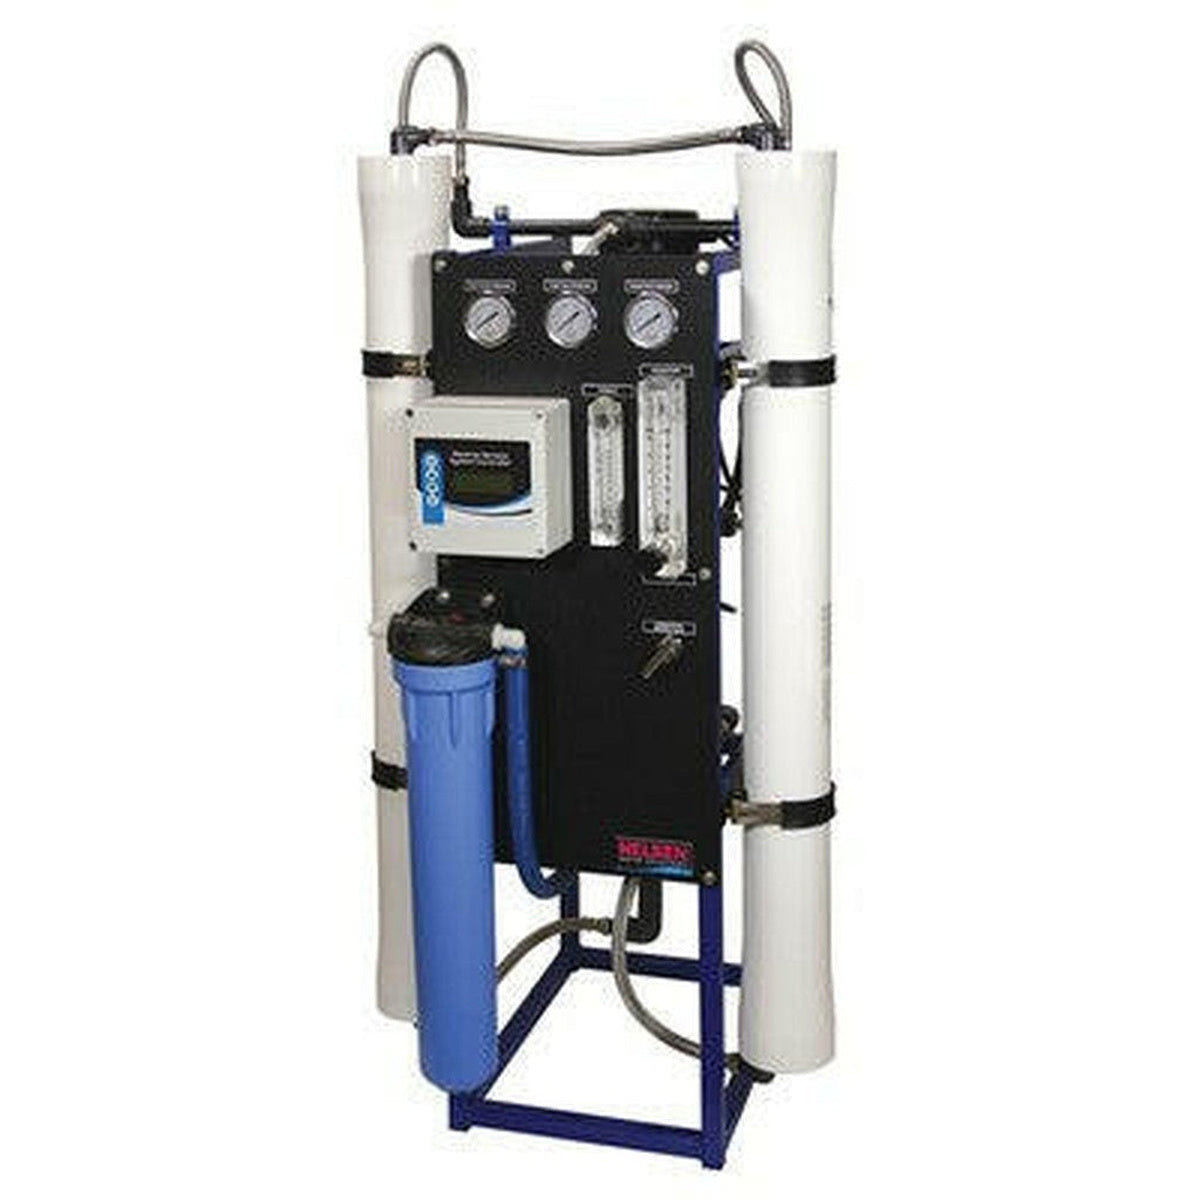
Addressing the Unique Water Characteristics of 68826 with Commercial Industrial Reverse Osmosis
The water source in the 68826 region presents a distinctive set of challenges that directly influence the choice and operation of commercial industrial reverse osmosis (RO) systems. Known for a combination of moderate total dissolved solids (TDS) and seasonal fluctuations in iron and manganese levels, local water demands equipment that is both resilient and adaptable. Understanding these factors is essential when selecting a reliable RO system tailored to the specific needs of industrial and commercial users in this area.
Local Water Chemistry and Its Impact on RO System Design
Water in the 68826 area typically exhibits moderate hardness, often ranging between 8 and 15 grains per gallon. This means calcium and magnesium content is high enough to pose scaling risks without appropriate pretreatment. Additionally, occasional spikes in naturally occurring iron—present in both dissolved and particulate forms—can accelerate membrane fouling and reduce system efficiency.
Moreover, manganese is commonly found alongside iron, and while it is less abundant, it compounds the challenge by staining membranes and pipelines, requiring effective filtration prior to the RO stage. Seasonal variances also bring varying levels of turbidity, particularly following rainfall or agricultural runoff, necessitating robust pretreatment filtration steps.
Choosing the Right Equipment Sizing for Industrial Demands
Industrial and commercial customers in 68826 often need RO systems capable of handling daily volumes ranging from several thousand to tens of thousands of gallons, depending on their business type. For example, food processing facilities or manufacturing plants generally require continuous, high-throughput systems with redundancy built in to minimize downtime.
When sizing an RO system, it is critical to factor in maximum daily water use, peak flows, and the local water quality variables. Oversizing can lead to unnecessary operational costs, while undersizing risks inadequate treatment and frequent maintenance headaches. Many systems in this area are configured with modular designs, allowing for future capacity expansion as operational needs evolve.
Essential Pretreatment to Protect RO Membranes
Given the iron and manganese content common in 68826 water, a thoroughly planned pretreatment stage is essential. This typically involves a combination of:
- Oxidation Filters: To convert dissolved iron and manganese into particulate form, making them easier to filter out.
- Greensand or Catalytic Media Filters: Specifically targeting iron and manganese removal before water reaches the RO membranes.
- Water Softeners or Anti-Scalant Dosing: To reduce hardness and protect membranes from scale formation, which can drastically reduce performance and membrane life.
- Cartridge Filtration: To remove sediment and any remaining particulate matter, particularly important if turbidity spikes seasonally.
Skipping or underestimating these steps can lead to frequent membrane fouling, increased downtime, and higher replacement costs.
Installation Considerations in the 68826 Area
Installation within this region should account for environmental and infrastructural factors typical of the local climate and building types. Seasonal temperature changes can affect both water temperature and system materials. For instance, extreme cold can cause freezing in uninsulated pipes, while high summer temperatures can impact membrane performance due to increased water temperature.
System housing or shelters that incorporate insulation and climate control help maintain stable operating conditions and extend equipment life. Additionally, space constraints common in older industrial buildings may require compact or modular RO designs that can fit neatly into available footprints without compromising capacity or ease of service.
Maintenance Interval Guidelines Tailored to Local Conditions
Maintenance frequencies for commercial industrial RO units in 68826 vary depending on water quality and system usage patterns, but typical practices include:
- Membrane Cleaning: Membranes should be inspected and cleaned every 4 to 6 months to remove scale, iron, and organic fouling. However, water samples showing higher iron or manganese levels might necessitate more frequent cleaning.
- Filter Replacement: Pretreatment filter media, such as greensand or catalytic filters, generally require media replacement or regeneration every 6 to 12 months based on iron load and flow rates.
- Pressure Vessel and Pump Checks: Regular inspections ensure seals, pressure vessels, and pumps are functioning optimally and not contributing to system inefficiencies or leaks.
- System Monitoring: Continuous monitoring of feedwater and permeate water quality, including TDS levels, pH, and pressure differentials, helps detect early signs of membrane degradation or pretreatment issues.
Adhering to a maintenance schedule adapted to the local water profile and system design significantly reduces unplanned downtime and extends the lifespan of the RO system components.
Why Locally Manufactured RO Systems Matter in 68826
Opting for USA-made commercial industrial RO systems offers practical advantages to operations within the 68826 area. Locally manufactured units tend to incorporate design features tailored to American water conditions and regulatory expectations, facilitating more effective performance.
Furthermore, proximity to manufacturing means faster access to replacement parts, specialized technical support, and customization options responsive to the unique treatment demands posed by the local water chemistry. This reliability and responsiveness can be critical in industrial contexts where water quality disruptions cause costly process interruptions.
Summary: Key Factors for Commercial RO Selection in 68826
- Anticipate fluctuating iron and manganese levels requiring robust pretreatment.
- Consider moderate hardness in the water; incorporate scale prevention methods.
- Choose equipment sized for peak demand with possible modular expansion.
- Provide system housing options that mitigate climate impacts.
- Institute maintenance plans aligned with local water chemistry variability.
- Favor USA-made systems to ensure compatibility, support, and parts availability.
By addressing these specific considerations, businesses in the 68826 region can optimize their commercial industrial reverse osmosis systems for consistent operation, reduced lifecycle costs, and sustained water quality that supports their production goals effectively.
Energy Efficiency Considerations for Commercial RO Systems
Energy consumption represents a significant operational cost for commercial reverse osmosis systems. In the 68826 region, businesses aiming to optimize their overall expenses should evaluate energy efficiency as a crucial factor when selecting or upgrading RO units.
Modern RO systems incorporate energy recovery devices such as pressure exchangers and turbines that capture and reuse pressure energy from the RO brine stream. This technology can reduce the energy requirements by up to 50%, particularly in high-recovery setups.
- Variable Frequency Drives (VFDs): Integrating VFDs with feedwater pumps allows the system to adjust flow rates dynamically, matching demand without unnecessary power consumption.
- System Automation: Automated control systems optimize operation schedules and prevent wasted energy during idle periods.
- High-Efficiency Pumps: Selecting pumps engineered for maximum hydraulic efficiency contributes to lower electrical input per unit of water produced.
Incorporating these energy-saving features not only reduces utility costs but also aligns with sustainability goals increasingly prioritized in industrial operations.
Advanced Pretreatment Strategies for Challenging Feedwater
While basic pretreatment protocols manage typical parameters like hardness and iron, complex water compositions in certain 68826 localities necessitate more sophisticated pretreatment approaches.
- Ultrafiltration (UF): UF membranes act as a physical barrier to suspended solids, bacteria, and colloidal matter, providing superior feedwater quality before the RO stage. This reduces membrane fouling and extends operational intervals between cleanings.
- Chemical Conditioning: Use of antiscalants, dispersants, and sequestering agents tailored to the feedwater chemistry prevents mineral scaling and biological growth on membranes.
- Oxidation-Reduction Techniques: Employing chlorination followed by dechlorination or advanced oxidation processes can control microbial contamination and organic compounds effectively.
Implementing these advanced pretreatment methods ensures the longevity and consistent performance of RO membranes in challenging water environments.
Membrane Types and Configurations for Industrial Applications
The choice of membrane material and configuration significantly impacts the suitability of RO systems for various industrial processes in 68826.
- Thin-Film Composite (TFC) Membranes: These are the industry standard for commercial RO due to their high rejection rates for dissolved solids, durability, and chemical resistance. They perform well under diverse feedwater conditions.
- Cellulose Triacetate (CTA) Membranes: While less common, CTA membranes offer better chlorine tolerance but slightly lower salt rejection. They may be preferred when residual chlorination is present.
- Spiral Wound Modules: The most prevalent membrane configuration, spiral wound modules provide a compact footprint and scalability for industrial water treatment.
- Hollow Fiber Membranes: Used primarily in ultrafiltration, these can be integrated as pretreatment or polishing steps within RO systems.
Selecting the appropriate membrane type tailored to feedwater characteristics and desired water quality ensures operational efficiency and durability.
System Integration and Automation Enhancements
Integrating commercial RO systems into existing plant operations can be significantly streamlined through process automation and system interconnectivity.
- SCADA Systems: Supervisory Control and Data Acquisition platforms allow real-time monitoring and control of RO plants. Operators can access performance data, receive alerts, and adjust parameters remotely.
- Predictive Maintenance Alerts: Advanced analytics software linked to sensors enables early detection of membrane fouling, scaling trends, or pump inefficiencies before failures occur.
- Automated Cleaning-in-Place (CIP): Automated CIP cycles reduce manual labor, optimize cleaning frequency, and help maintain membrane flux and rejection rates.
Enhancing RO systems with automation tools improves reliability, reduces human error, and optimizes resource utilization in industrial settings.
Wastewater Management and Brine Disposal Solutions
RO processes generate a concentrated brine byproduct that must be managed responsibly to comply with environmental regulations and minimize ecological impact.
- Zero Liquid Discharge (ZLD) Systems: These advanced treatment trains further concentrate RO brine to recover water and valuable salts, producing dry solid waste that is easier to handle.
- Evaporation Ponds: In some industrial settings, properly designed evaporation ponds provide a natural disposal method for brine, taking into account local climate and soil conditions.
- Injection Wells: Deep well injection can be employed where permitted to safely isolate concentrate streams underground.
- Brine Concentrators: Mechanical evaporation or membrane concentrators reduce brine volume before final disposal.
Choosing an appropriate brine management strategy depends on plant size, local discharge regulations, and environmental sustainability goals.
Customizable System Design for Varied Industrial Needs
Different industries in the 68826 region impose unique water treatment requirements that demand versatile RO system designs.
- Food and Beverage: Requires stringent removal of impurities while maintaining mineral balance suitable for product formulations.
- Pharmaceutical Manufacturing: Necessitates ultra-pure water with minimal endotoxins and organics.
- Power Generation: Emphasizes scale-free high-purity water to protect turbines and boilers.
- Chemical Processing: Demands consistent water quality to ensure product consistency and process safety.
RO system manufacturers often provide tailored solutions incorporating specialty materials, multilayer filtration stages, and precise control schemes to meet these sector-specific challenges.
Environmental Considerations and Regulatory Compliance
Commercial RO operations must adhere to federal, state, and local environmental standards relating to discharge quality, chemical handling, and energy consumption.
- EPA Guidelines: Ensuring RO brine and wastewater meet effluent standards before release.
- OSHA Safety Standards: Proper handling and storage of chemicals used in pretreatment and cleaning protocols.
- Water Conservation Initiatives: Employing high recovery rates and water reuse strategies to minimize freshwater intake.
- Periodic Reporting: Maintaining accurate water quality and operational logs to demonstrate compliance during audits.
Proactive engagement with regulatory frameworks helps prevent costly penalties and supports corporate sustainability objectives.
Related
- Commercial Industrial Reverse Osmosis Usa Made 30217
- Commercial Industrial Reverse Osmosis Usa Made 32358
- Commercial Industrial Reverse Osmosis Usa Made 32506
- Commercial Industrial Reverse Osmosis Usa Made 33570
- Commercial Industrial Reverse Osmosis Usa Made 33920
- Commercial Industrial Reverse Osmosis Usa Made 35031
- Commercial Industrial Reverse Osmosis Usa Made 35055
Water Softener Plus Industrial Reverse Osmosis System — 4800 GPD
This system is configured to order. Send a quote request and we will come back with sizing, freight and a firm price for your water.
See full specifications