
Commercial Industrial Reverse Osmosis Usa Made 58008

Pricing: request a quote
Get a QuoteWater Softener Plus Industrial Reverse Osmosis System — 4800 GPD
✓ Free shipping in the USA · ✓ 90-day returns · ✓ Secure checkout
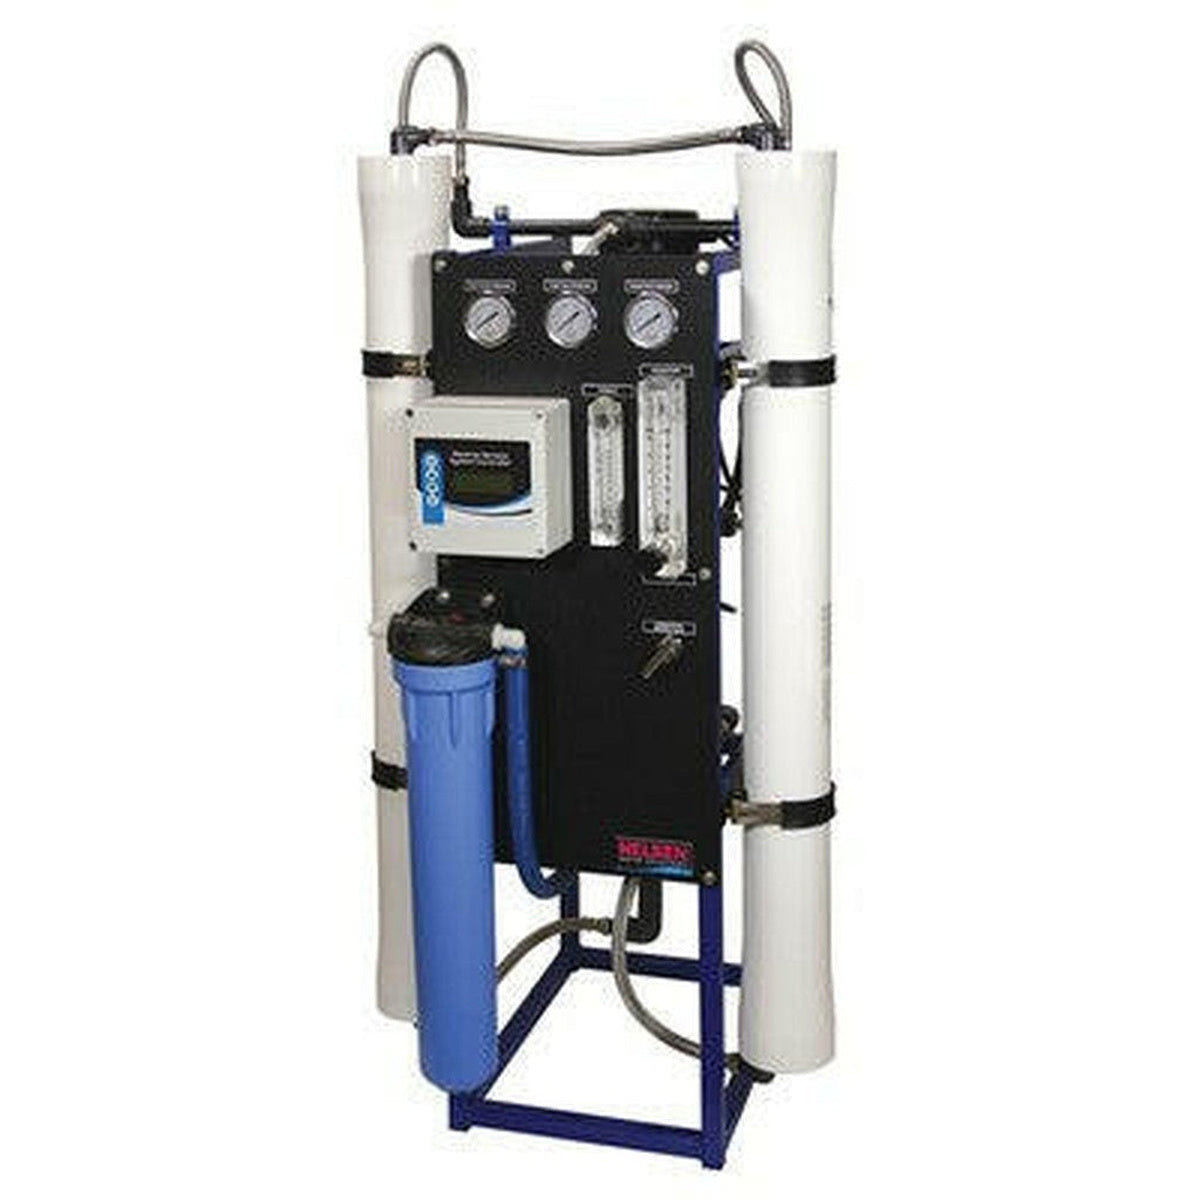
Addressing the Unique Water Conditions of the 58009 Area with Commercial Industrial Reverse Osmosis Systems
The water in the 58009 region is notable for its combination of seasonal fluctuations in mineral content and relatively high levels of silica and iron. These characteristics pose distinct challenges for commercial and industrial reverse osmosis (RO) applications, making system selection and maintenance critical for long-term efficiency and water quality.
Water Chemistry Factors Impacting RO Performance in 58009
Unlike regions with predominantly hard water caused by calcium and magnesium, 58009’s water profile frequently shows moderate hardness accompanied by elevated silica concentrations and iron in both dissolved and particulate forms. Silica in particular can cause scaling issues on membrane surfaces that are less common in other areas, requiring specific pre-treatment steps.
- Hardness Levels: Typically moderate, but variable depending on seasonal runoff, hardness contributes to calcium carbonate scaling potential.
- Silica Presence: Silica tends to accumulate on membranes and piping, reducing permeate flow if not properly managed.
- Iron Content: Iron can oxidize and foul membranes, necessitating iron removal methods prior to RO filtration.
- Total Dissolved Solids (TDS): Generally moderate, but spikes during certain periods underline the need for flexible system design.
System Sizing and Capacity Considerations for 58009
When selecting a commercial or industrial RO unit for this ZIP code, it's important to account for these water chemistry fluctuations. System sizing should not only reflect the average daily water demand but also accommodate peak needs and varying water quality conditions.
For facilities with intermittent usage or seasonal operation changes, modular RO systems with scalable capacities offer adaptability. Additionally, installing pre-treatment equipment designed to handle iron and silica challenges helps protect RO membranes and extends system lifespan, allowing for consistent output.
Pre-Treatment Strategies Essential for Reliable Operation
Effective pre-treatment is essential to minimize membrane fouling and scaling. In the 58009 area, these strategies usually include:
- Iron Removal: Aeration followed by filtration or chemical oxidation can significantly reduce iron concentrations before RO feedwater.
- Silica Control: Using coagulation and media filtration prior to RO reduces dissolved silica, mitigating scale buildup.
- Water Softening: Depending on hardness fluctuations, ion-exchange softening may be necessary to prevent calcium carbonate scaling.
- Carbon Filtration: Removes chlorine or chloramine residuals that can damage RO membranes.
Maintenance Intervals and Operational Considerations
In this region, maintaining RO system performance means regular monitoring and proactive maintenance tailored to local water conditions.
- Membrane Cleaning: Due to silica and iron fouling risks, cleaning cycles may need to be more frequent than in areas without these contaminants.
- Pre-Treatment Media Replacement: Filtration media used for iron and silica removal should be inspected and replaced according to usage and contaminant load.
- System Monitoring: Routine checks for pressure differentials, permeate flow, and water quality parameters ensure early detection of membrane fouling or pre-treatment inefficiencies.
- Pump and Valve Maintenance: These mechanical components should be serviced regularly to prevent downtime and maintain consistent throughput.
Installation Considerations Tailored to Commercial and Industrial Settings
Installing a commercial or industrial RO system in the 58009 area involves careful planning to address local water variability and operational demands.
- Site-Specific Water Testing: Comprehensive water analysis prior to installation ensures the system design matches the unique chemistry challenges.
- Pre-Treatment Equipment Placement: Proper spatial layout facilitates easy maintenance access and optimizes flow dynamics.
- Allowance for Expansion: Anticipating future capacity increases by choosing modular systems or reserving space supports long-term operational flexibility.
- Integration with Existing Infrastructure: Seamless connection to current water lines and waste management systems reduces installation complexity and downtime.
Why Choosing USA-Made Commercial RO Systems Matters in 58009
Opting for USA-made RO equipment ensures adherence to rigorous manufacturing standards, an important consideration given the demands placed on systems by the 58009 water profile. These units often feature components certified for consistent quality and ease of replacement, which supports efficient maintenance and reliability.
Moreover, domestic manufacturing typically enables faster access to technical support and replacement parts, minimizing downtime when water quality issues or system wear require prompt attention.
Conclusion: Tailoring Reverse Osmosis Solutions to Local Water Realities
For commercial and industrial users in the 58009 area, water treatment solutions must confront the dual challenges of variable hardness and elevated silica and iron levels. Carefully sized systems with robust pre-treatment, combined with attentive maintenance schedules and strategic installation planning, form the foundation of effective reverse osmosis water purification in this region.
Choosing equipment crafted to meet these specific local water conditions, such as USA-manufactured commercial RO units, further supports sustainable operation and consistent water quality, ultimately protecting processes and infrastructure dependent on clean water.
Advanced Monitoring and Control Systems for Commercial RO Plants
Modern commercial reverse osmosis systems in the 58009 region benefit significantly from integrated monitoring and control technologies. These systems enable real-time data acquisition and automated adjustments that help maintain optimal performance despite fluctuating feed water conditions.
- Automated Pressure and Flow Sensors: Sensors continuously measure feed water pressure, permeate flow rates, and concentrate flow, allowing for immediate detection of anomalies such as membrane fouling or scaling. This real-time feedback facilitates proactive maintenance interventions, reducing downtime and extending membrane life.
- Conductivity and TDS Monitoring: Inline conductivity sensors monitor total dissolved solids (TDS) levels in both feed water and permeate. Sudden changes can indicate membrane breaches or changes in feed water quality, triggering alarms or system adjustments to maintain water purity.
- SCADA and Remote Access: Supervisory Control and Data Acquisition (SCADA) systems enable centralized control and continuous monitoring across multiple RO units or sites. Remote access capabilities allow operators to oversee system performance and make adjustments without being physically present, improving response times and operational efficiency.
Energy Recovery Technologies in Water Treatment
Given the energy-intensive nature of reverse osmosis, implementing energy recovery devices (ERDs) can greatly improve system efficiency, reduce operational costs, and lessen environmental impact, which is especially valuable in the commercial sector.
- Pressure Exchangers: These devices reclaim high-pressure brine energy and transfer it to incoming feed water, significantly lowering the power required for pressurization. This technology is particularly effective in large-scale RO plants where brine pressures can be harnessed efficiently.
- Turbochargers and Pelton Turbines: These rotary energy recovery devices convert the energy from high-pressure concentrate into mechanical energy to assist feed water pressurization. They are robust and commonly used in commercial systems that treat moderate to high salinity waters.
- Impact on Carbon Footprint: By reducing the energy consumption of the RO system, energy recovery devices contribute to lower greenhouse gas emissions associated with water treatment, an increasing priority for environmentally conscious businesses in 58009.
Membrane Cleaning and Longevity Strategies
Maintaining membrane integrity and performance is critical to sustaining water quality and controlling operating expenses over the lifespan of an RO system. Advanced cleaning protocols and membrane care techniques are central to this goal.
- CIP (Cleaning-In-Place) Systems: Automated cleaning cycles utilizing chemical cleaners tailored to the local water chemistry prevent buildup of iron, silica, and biological fouling. CIP systems reduce manual labor and ensure thorough membrane cleaning without system disassembly.
- Cleaning Chemicals Selection: Selecting appropriate acid, alkaline, and biocide cleaners based on water analysis and fouling type optimizes cleaning efficacy while minimizing chemical consumption and membrane degradation.
- Routine Membrane Integrity Testing: Techniques such as pressure decay tests and salt rejection measurements help detect early signs of membrane damage or fouling, enabling timely replacements or adjustments to cleaning frequency.
Addressing Seasonal Variations in Water Quality
Fluctuations in raw water quality due to seasonal changes pose unique challenges to RO systems. Strategies to adapt operations ensure consistent output despite variability.
- Dynamic Pretreatment Adjustments: Adjusting coagulation, filtration, and chemical dosing schedules in response to seasonal organic load and turbidity changes preserves membrane performance.
- Adaptive Operating Parameters: Modifying recovery rates, feed pressure, and flushing cycles seasonally mitigates the risk of scaling or membrane fouling under changing feed water conditions.
- Water Source Monitoring: Increased sampling and analysis during transitional periods allow for early identification of shifts in contaminants, supporting proactive system tuning.
Waste Brine Management and Environmental Compliance
Managing the reject water, or brine, produced by RO systems is crucial to minimizing environmental impact and meeting regulatory requirements in the 58009 area.
- Volume Reduction Techniques: Employing techniques such as evaporation ponds, zero liquid discharge (ZLD) systems, or brine concentrators can reduce the volume of waste discharged, lowering disposal costs and environmental footprint.
- Safe Disposal Practices: Coordinating with local wastewater treatment facilities and adhering to discharge permits ensure that brine disposal does not negatively affect local ecosystems.
- Potential for Resource Recovery: Innovative approaches are increasingly focusing on recovering valuable minerals such as silica or calcium salts from concentrate streams, turning waste into usable by-products.
Training and Operator Expertise for Optimal System Performance
Well-trained operators are essential for the smooth operation and longevity of commercial RO systems. Ongoing education ensures that staff can handle complex troubleshooting, maintenance, and optimization tailored to local conditions.
- Comprehensive Training Programs: Covering system design principles, water chemistry influences, equipment operation, and emergency response empowers operators to maintain optimum system performance.
- Regular Skill Updates: Periodic refresher courses incorporating the latest RO technologies, regulatory changes, and best practices help maintain high proficiency levels.
- Operator Involvement in Data Analysis: Engaging operators in reviewing monitoring data and performance trends supports informed decision-making and early detection of anomalies.
Innovations in Membrane Materials and Configurations
The rapidly evolving field of membrane technology offers new opportunities for improved performance in commercial RO systems operating in challenging environments like 58009.
- Thin-Film Composite Membranes: Enhanced permeability and selectivity characteristics improve water recovery rates while maintaining high contaminant rejection, reducing energy demand.
- Anti-Fouling Coatings: Advanced surface treatments reduce biofouling and scaling tendencies, lowering chemical cleaning frequency and extending membrane life.
- Flexible Membrane Configurations: High-recovery and low-recovery hybrid arrangements allow system customization to balance permeate quality, energy consumption, and concentrate volume.
Customized Service Agreements and Lifecycle Support
Long-term partnerships with RO system providers can deliver sustainable value through tailored service agreements addressing maintenance, upgrades, and technical support.
- Preventive Maintenance Contracts: Scheduled inspections, component replacements, and cleaning services ensure consistent operation and help avoid costly emergency repairs.
- System Performance Audits: Periodic comprehensive reviews analyze operational data, identifying optimization opportunities and informing upgrade decisions.
- Upgrade and Retrofit Services: Providers offer solutions for integrating emerging technologies or expanding capacity without complete system replacement, preserving investment while enhancing performance.
Regulatory Considerations and Compliance for Commercial Water Treatment
Operating commercial RO systems within the regulatory framework applicable to the 58009 area ensures safety, environmental stewardship, and avoidance of penalties.
- Water Quality Standards: Compliance with federal and state drinking water and wastewater discharge standards dictates system design parameters and monitoring protocols.
- Permitting and Reporting: Obtaining required permits for water intake, chemical use, and waste disposal typically involves regular sampling and documentation to demonstrate compliance.
- Worker Safety Regulations: Adherence to OSHA guidelines for chemical handling, confined space entry, and equipment operation protects personnel involved in system maintenance.
Related
- Commercial Industrial Reverse Osmosis Usa Made 30217
- Commercial Industrial Reverse Osmosis Usa Made 32358
- Commercial Industrial Reverse Osmosis Usa Made 32506
- Commercial Industrial Reverse Osmosis Usa Made 33570
- Commercial Industrial Reverse Osmosis Usa Made 33920
- Commercial Industrial Reverse Osmosis Usa Made 35031
- Commercial Industrial Reverse Osmosis Usa Made 35055