
Choosing the Right Water Treatment for Hard Water in Your Commercial Bakery
Pricing: request a quote
Get a QuoteNelsen 120,000 Grain Twin-Tank Commercial (NWS20) Water Softener
✓ Free shipping in the USA · ✓ 90-day returns · ✓ Secure checkout

The Challenge of Hard Water in a Commercial Bakery Setting
As an owner or operator of a bakery operating on well water, you face unique challenges from hard water. The presence of minerals like calcium and magnesium in your water supply causes chalky residue buildup on surfaces and appliances. This buildup can stiffen laundry, affect dough quality, and lead to early wear and tear on equipment critical to your baking process. These symptoms threaten your ability to deliver consistent product quality and can increase maintenance downtime, impacting your daily operations and customer satisfaction.
Your bakery's high water demand, driven by long operating hours and continuous production cycles, intensifies these issues. Ensuring uninterrupted service while managing labor costs associated with cleaning and equipment replacement is a key concern. The decision you face is determining which type of water treatment can deliver reliable, high-capacity performance tailored to your commercial environment, safeguarding your investment and your bakery’s reputation.
Exploring Water Treatment Classes and How They Work
When addressing hard water in commercial bakeries, several classes of treatment are commonly considered. Each operates through a different mechanism to reduce the impact of minerals on water.
- Water Conditioners: These alter the behavior of dissolved minerals to prevent scale buildup without removing the hardness ions. They often rely on physical or chemical methods to keep minerals dispersed.
- Water Softeners: These exchange hardness minerals for sodium or potassium ions through an ion exchange process, effectively removing the minerals responsible for scaling.
- Reverse Osmosis Systems: These use a membrane to remove a wide range of contaminants, including hardness minerals, producing very pure water but typically with lower throughput and higher waste water.
- Magnetic or Electronic Descalers: These claim to prevent scale by modifying mineral crystal structures via magnetic or electric fields but provide inconsistent results in commercial settings.
Why Several Treatment Classes Are Unsuitable Here
In a commercial bakery with high demand and well water sources, not all treatment options meet your requirements.
- Water Conditioners do not physically remove hardness minerals. While they may reduce scale buildup to some extent, the chalky residue often still appears, affecting equipment and surfaces. This incomplete treatment risks equipment warranty violations and does not fully protect against downtime.
- Reverse Osmosis Systems
- Magnetic or Electronic Descalers lack consistent performance under commercial loads and hard water concentrations. The scientific support for their effectiveness is limited, making them unreliable for critical bakery operations where continuous, predictable water quality is essential.
These elimination steps narrow your viable options, focusing on solutions that guarantee mineral removal to ensure equipment longevity, consistent baking quality, and compliance with operational standards.
Essential Performance Attributes for Effective Hard Water Treatment Here
Given your bakery’s operational demands, the ideal water treatment system must deliver several key attributes:
- Complete Hardness Ion Removal: Prevent mineral buildup that can cause equipment damage and product quality issues.
- High Capacity and Continuous Operation: Accommodate your bakery’s water volume throughout trading hours without deterioration in performance or frequent downtime.
- Reliability and Ease of Management: Enable straightforward handling with minimal labour for maintenance and water quality assurance, limiting interruption risks.
- Durability Suitable for Well Water: Handle naturally occurring well water characteristics without premature wear or failure.
Systems meeting these criteria protect your bakery’s operational workflow and product standards, while addressing labor and warranty concerns effectively.
Proven Water Softening Solution for Commercial Bakery Hard Water
Among treatment options designed to meet commercial demands, one approach stands out: the softener class that uses ion exchange technology. This method thoroughly removes the minerals responsible for hard water symptoms and maintains consistent water quality under heavy load conditions.
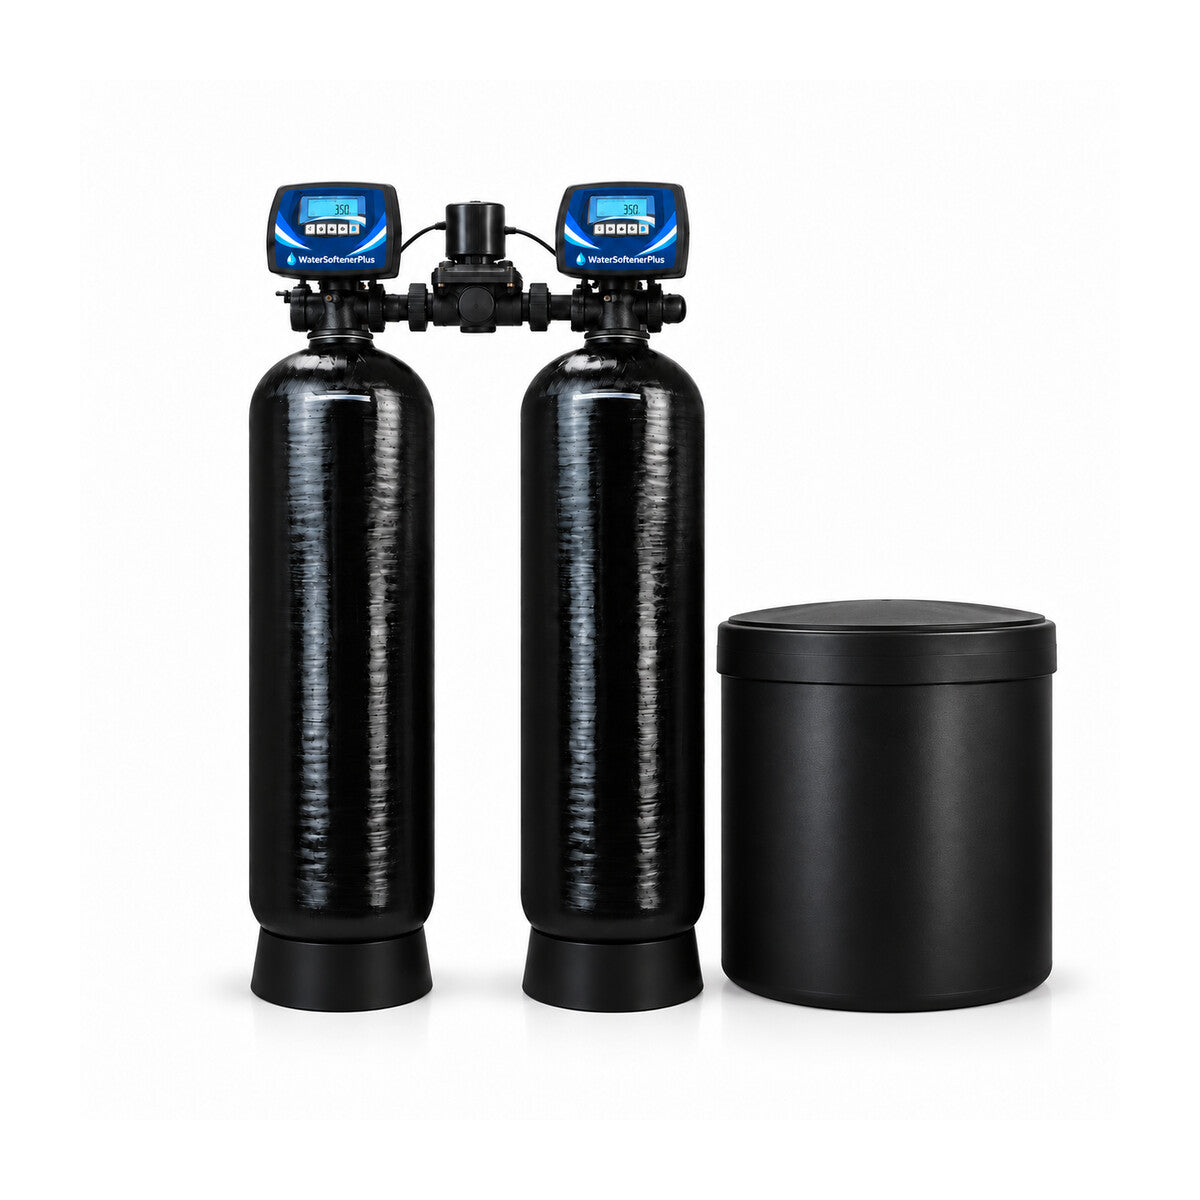
A documented example that aligns with these requirements is the Nelsen 120,000 Grain Twin-Tank Commercial Water Softener by NWS. This unit features a twin-tank design, allowing for continuous service during regeneration cycles, which is crucial for commercial settings like your bakery.
With a grain capacity of 120,000 and twin 24x41 inch tanks, this system supports high throughput aligned with your bakery’s operational hours, minimizing downtime and labor demands. It ships ready to configure, facilitating a smooth transition to softened water that reduces chalky residue on equipment and laundry stiffness, ultimately extending the life of your appliances and improving product consistency.
Selecting a solution within this treatment class tailored to your water quality and usage guarantees the necessary performance, reliability, and compliance that your bakery requires.
Nelsen 120,000 Grain Twin-Tank Commercial (NWS20) Water Softener
Priced on request for your specification.