
Commercial Industrial Reverse Osmosis Usa Made 87014

Pricing: request a quote
Get a QuoteWater Softener Plus Industrial Reverse Osmosis System — 4800 GPD
✓ Free shipping in the USA · ✓ 90-day returns · ✓ Secure checkout
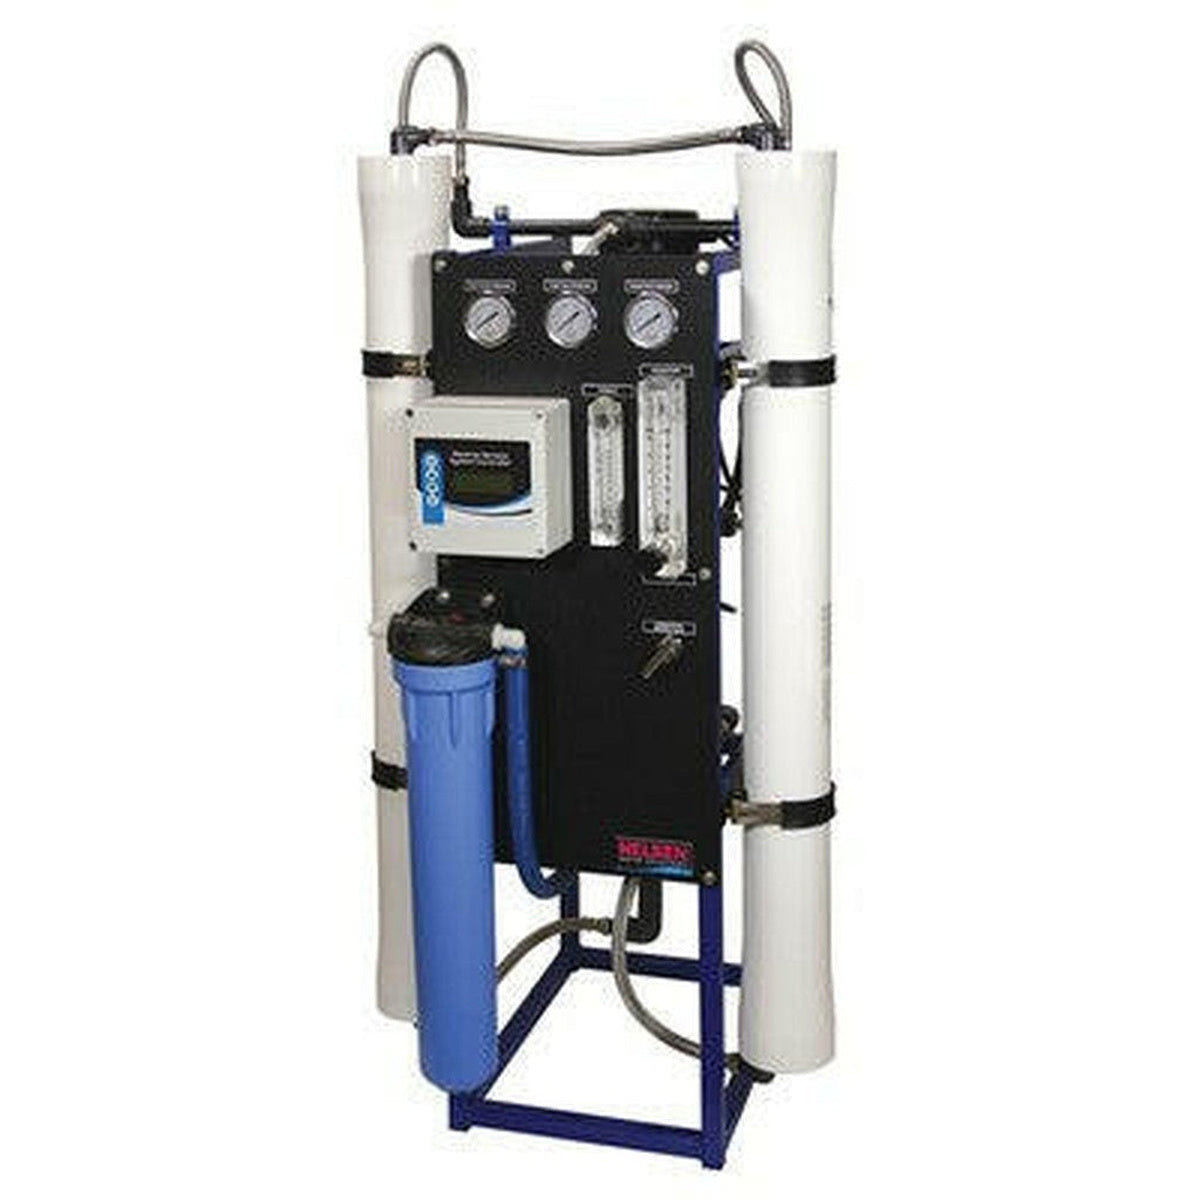
Addressing Local Water Characteristics in the 87015 Area for Industrial Reverse Osmosis
The water in the 87015 region exhibits a unique chemical profile that directly influences the performance and maintenance needs of commercial industrial reverse osmosis (RO) systems. This area’s groundwater typically features a moderate to high level of dissolved minerals, including calcium and magnesium, resulting in moderately hard water that can accelerate scaling on RO membranes if not properly managed. Understanding the specific water chemistry here is critical when selecting and maintaining a robust RO system.
Local Water Composition and Its Impact on Reverse Osmosis Equipment
Water sourced in 87015 tends to have elevated levels of total dissolved solids (TDS), often including naturally occurring elements such as sulfate and chloride ions. These components can contribute to osmotic pressure challenges and may reduce membrane efficiency over time. Iron and manganese, while generally found in low concentrations, can occasionally present issues by staining equipment and fouling membranes if pretreatment is inadequate.
Moreover, the pH of the water in this area often ranges near neutral but can fluctuate slightly toward acidic or basic, depending on seasonal rainfall and groundwater recharge patterns. These pH shifts require careful system balancing to prevent membrane degradation and maintain optimal rejection rates.
Sizing Considerations for Industrial RO Systems in 87015
When determining equipment size for commercial use in this region, it's important to account for both the flow rate required and expected feedwater variability. Plants in the 87015 area typically handle flows ranging from several hundred to a few thousand gallons per day, but larger industrial operations may require systems designed to process significantly higher volumes.
- Flow demand assessment: Estimating peak daily usage ensures the RO system can consistently meet operational needs without excessive strain.
- System scalability: Modular designs benefit these operations by allowing incremental capacity increases if water usage grows or water quality changes.
- Pre-filtration stage sizing: Given local sediment and particulate levels, sufficient pre-treatment filtration must precede the RO membranes to prevent clogging and extend membrane life.
Installation Factors Unique to 87015 Water Sources
Installation practices in this region must take into account the mineral composition and the presence of iron and manganese. Proper site assessment is essential to identify iron-related fouling risks that could hinder RO membrane function. Installation in areas with variable groundwater levels may also necessitate flexible intake designs to accommodate changing water tables.
Accessibility for routine maintenance is a key consideration, as the mineral-rich water can accelerate membrane fouling and scaling, requiring more frequent intervention. Positioning the system near power sources and integrating appropriate monitoring devices will help maintain optimal performance.
Maintenance Protocols Adapted for 87015 Water Conditions
Given the tendency for scaling and potential fouling due to the local water chemistry, maintenance intervals should be scheduled more frequently than systems installed in softer water locations. Key maintenance tasks include:
- Regular membrane cleaning: Chemical cleaning tailored to remove calcium carbonate scale and biofilms can preserve membrane permeability and efficiency.
- Routine replacement of pre-filters: Sediment and carbon filters should be monitored and replaced based on pressure drop readings rather than fixed schedules to prevent particulate breakthrough.
- Water quality monitoring: Periodic testing of feedwater and product water for TDS, pH, and specific ion concentrations helps detect trends that may indicate membrane degradation or pretreatment issues.
- Inspection of pumps and valves: Ensuring that auxiliary equipment is functioning correctly prevents system downtime and supports steady operating pressure essential for consistent RO performance.
Treating Hardness and Scaling Potential Before Reverse Osmosis
Although reverse osmosis membranes reduce hardness to very low levels, high feedwater hardness requires pretreatment to avoid rapid scale formation. Ion exchange softeners or antiscalant dosing systems are common solutions in this area. The choice depends on operation scale and regulatory preferences:
- Ion exchange softening: Effective in removing calcium and magnesium ions, softening reduces the chance of scale but requires regeneration processes and salt management.
- Antiscalant chemical dosing: Useful when softening is impractical, these chemicals inhibit scale formation by interfering with crystal growth on membranes.
Careful analysis of water chemistry from the 87015 region aids in optimizing pretreatment selection and dosage rates to balance performance and ongoing operational costs.
Addressing Iron and Manganese Fouling Risks
Instances of iron and manganese presence in the 87015 water supply, while typically low, need special attention because these minerals oxidize and precipitate, causing membrane fouling and staining of components. Steps to mitigate these risks include:
- Oxidation and filtration: Introducing aeration or chemical oxidants followed by filtration removes dissolved iron and manganese before they reach the RO membranes.
- Periodic cleaning protocols: Employing cleaning solutions effective against metal oxide deposits maintains membrane flux and water quality.
Failing to address these elements in pretreatment can lead to frequent membrane replacement and increased operational downtime.
Considerations for Long-Term System Efficiency
Systems installed in the 87015 locale require a holistic approach focused on balancing water treatment complexity and maintenance effort. Implementing comprehensive monitoring systems that track pressure differentials, flow rates, and water quality parameters allows early identification of potential problems and timely interventions.
Regular training for operators on local water chemistry effects and system response prepares facilities for addressing issues promptly, reducing unplanned outages and extending the life of expensive RO membranes.
Optimizing Energy Use for Reverse Osmosis in 87015
The energy consumption of industrial RO systems is influenced by feed water characteristics and system design choices. The relatively high TDS typical in the 87015 groundwater means higher feed pressure is often necessary to overcome osmotic pressure. To achieve energy efficiency:
- Consider energy recovery devices where applicable, especially in large-scale systems.
- Maintain component condition to reduce friction losses and leaks.
- Design systems with variable speed controls to adapt pumping power to actual load.
These strategies help minimize operational costs while maintaining consistent output quality.
Summary: Tailoring Reverse Osmosis Systems for 87015 Water Demands
Commercial industrial RO installations in the 87015 area must be sized and designed with attention to the moderately hard, mineral-rich water common to this region. Pretreatment to manage hardness, iron, and manganese is essential to prolong membrane lifespan and maintain system efficiency. Scheduled preventative maintenance that includes cleaning, monitoring, and filter replacement is critical given local water characteristics. Thoughtful installation planning addressing site-specific water variability and accessibility further ensures reliable, long-term performance.
Advanced Pretreatment Techniques for Challenging Water Composition
Beyond standard pretreatment strategies, 87015 water requires advanced solutions to manage specific contaminants and improve overall RO system performance. Addressing issues like silica scaling, biofouling, and organic compounds demands tailored approaches that complement routine hardness and iron removal.
Silica Control
Silica, present in varying concentrations in the region’s groundwater, poses a risk for irreversible scaling on RO membranes, especially under high recovery operations. Traditional acid dosing combined with specialized antiscalants targeting silica polymerization helps mitigate these effects. Additionally, incorporating ion exchange or lime softening as pretreatment steps reduces silica concentration before the feed water reaches the membranes.
Biofouling Prevention
Biological growth within RO systems accelerates membrane degradation and decreases throughput. To combat this, advanced pretreatment includes:
- Ultraviolet (UV) disinfection units to reduce microbial load without chemical residues
- Periodic chlorination with dechlorination prior to membrane entry to inhibit bacterial proliferation
- Use of biodegradable antiscalants and biocides compatible with RO membranes
Incorporating these methods maintains membrane surface integrity and minimizes the frequency of chemical cleaning cycles.
Organics and Color Removal
Natural organic matter (NOM) and color-causing compounds, though less prominent, can influence RO system hydraulics and fouling potential. Employing enhanced coagulation-flocculation pretreatment technologies, coupled with high-performance filtration media, ensures effective removal of these components, safeguarding downstream membranes and improving permeate quality.
Innovative Membrane Materials and Configurations
The technological evolution of RO membranes offers options better suited for localized water characteristics and operational goals in 87015.
Thin-Film Composite (TFC) Membranes with Fouling Resistance
Recent developments feature membranes with surface modifications that reduce organic and biofilm adherence, extending operational duration between cleanings. These membranes often incorporate hydrophilic coatings or antimicrobial agents that inhibit biofouling without compromising salt rejection.
Hybrid Membrane Systems
Combining RO membranes with nanofiltration (NF) or ultrafiltration (UF) membranes can optimize pretreatment by removing specific contaminants more effectively upstream. For example, integrating a UF layer reduces suspended solids and microbial content, decreasing stress on RO membranes.
Membrane Module Orientation and Configuration
Selecting appropriate module arrangements such as spiral wound, hollow fiber, or plate-and-frame designs can influence cleaning efficiency, recovery rates, and footprint. Spiral wound modules remain standard due to cost-effectiveness, but plate-and-frame systems offer easier access for thorough cleaning in systems prone to severe fouling.
Water Recovery Optimization and Brine Management
Maximizing water recovery while managing concentrate disposal is critical in the semi-arid 87015 area, where water conservation is a priority and environmental regulations are stringent.
Enhanced Recovery Strategies
- Employing staged RO systems with multiple passes to increase recovery without excessive membrane fouling
- Integrating permeate flushing to reduce fouling and maintain consistent flow.
- Utilizing real-time sensors to dynamically adjust operating pressures and recovery rates based on feed water variability
Brine Concentrate Handling
Proper disposal or treatment of brine concentrate is essential to avoid environmental harm. Strategies include:
- Evaporation ponds designed with liners and monitoring to minimize seepage and contamination
- Zero liquid discharge (ZLD) systems combining RO with thermal evaporation and crystallization to recover salts and water simultaneously
- Co-treatment of brine with municipal wastewater streams where feasible, diluting concentrate prior to discharge
- Exploring beneficial reuse options such as salt harvesting or use in industrial processes requiring saline inputs
Automation and Remote Monitoring Enhancements
Advances in digital control systems allow RO installations to operate more efficiently, especially in hard-to-access or unattended settings, common in rural areas of 87015.
Smart Sensors and Predictive Analytics
Integration of advanced sensors measuring parameters like pH, conductivity, turbidity, and oxidation-reduction potential (ORP) provides granular insight into water quality trends and membrane status. Coupling this data with machine learning algorithms enables predictive maintenance scheduling and anomaly detection before failures occur.
Remote Operation and Troubleshooting
Using IoT platforms and cloud connectivity, operators can monitor system health, adjust setpoints, and initiate cleaning cycles remotely. This capability reduces onsite labor demands and permits rapid response to issues, critical for maintaining continuous operation in industrial contexts.
Automated Chemical Dosing
Dynamic dosing control based on real-time water chemistry metrics optimizes reagent use, reducing waste and operational costs while ensuring effective scale and fouling management.
Environmental and Regulatory Compliance Considerations
RO system deployment must align with local environmental regulations governing water withdrawal, concentrate discharge, and chemical storage.
Compliance Planning and Reporting
Comprehensive documentation of water sources, treatment efficacy, and discharge quality supports permit acquisition and renewal processes. Routine sampling programs, supported by automated data logging, facilitate transparent reporting and stakeholder confidence.
Sustainable Water Management Practices
- Implementing water reuse strategies within industrial operations to reduce freshwater withdrawals
- Minimizing chemical usage through optimized pretreatment and membrane cleaning protocols
- Employing lifecycle assessments to quantify and reduce environmental footprints across system components
Related
- Commercial Industrial Reverse Osmosis Usa Made 30217
- Commercial Industrial Reverse Osmosis Usa Made 32358
- Commercial Industrial Reverse Osmosis Usa Made 32506
- Commercial Industrial Reverse Osmosis Usa Made 33570
- Commercial Industrial Reverse Osmosis Usa Made 33920
- Commercial Industrial Reverse Osmosis Usa Made 35031
- Commercial Industrial Reverse Osmosis Usa Made 35055