
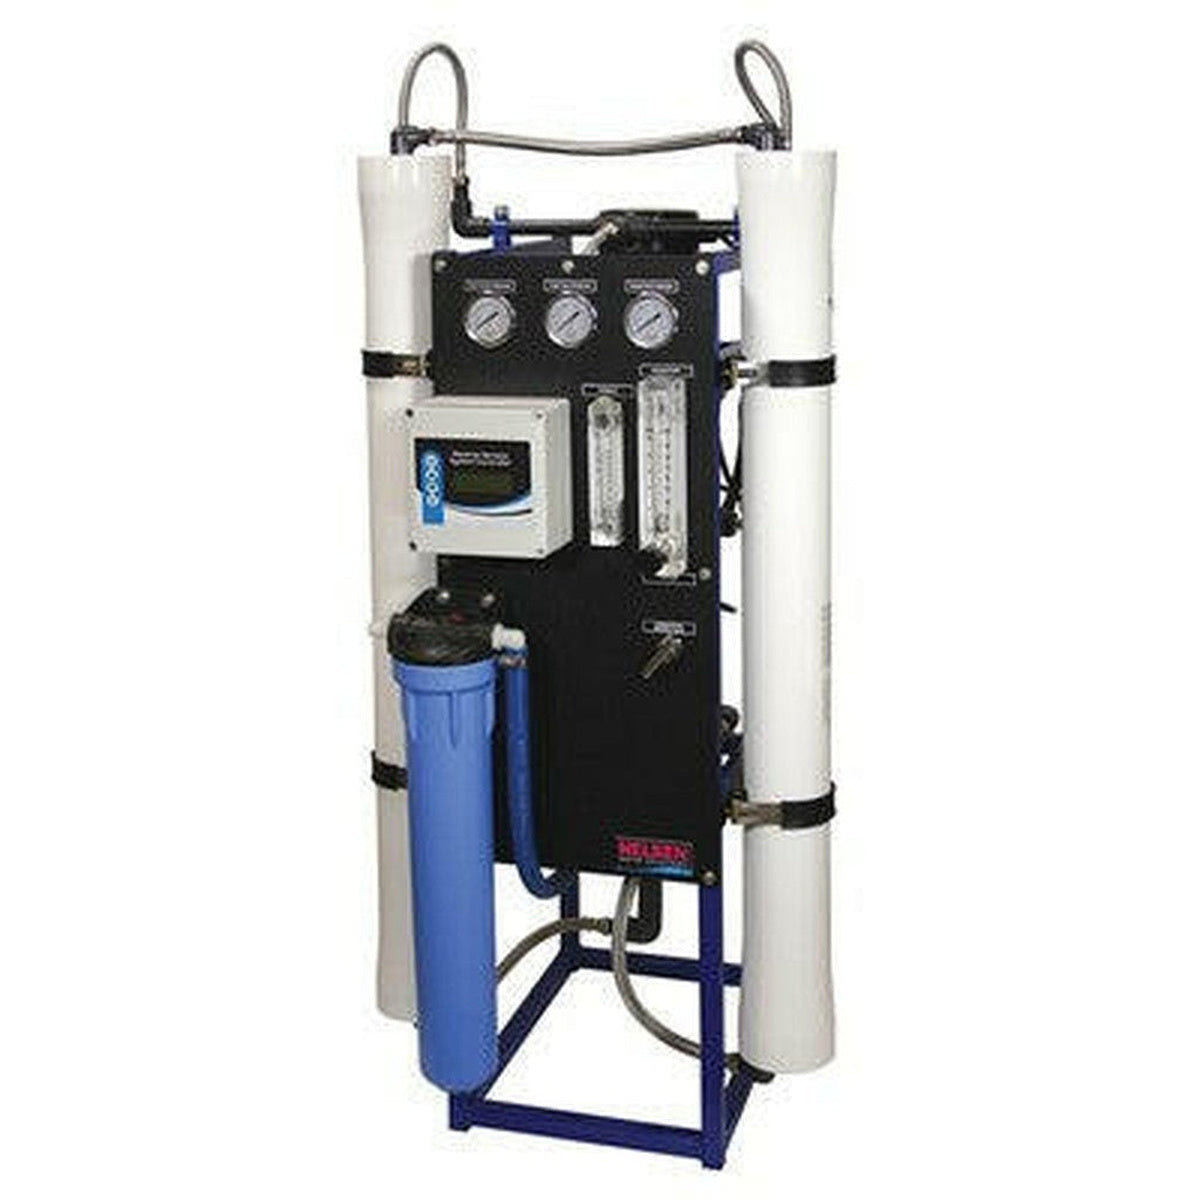
Commercial Industrial Reverse Osmosis Usa Made 43338

Pricing: request a quote
Get a QuoteWater Softener Plus Industrial Reverse Osmosis System — 4800 GPD
✓ Free shipping in the USA · ✓ 90-day returns · ✓ Secure checkout
Industrial Reverse Osmosis Solutions Suited for 43339 Water Conditions
The water supply in the 43339 area typically exhibits a mix of moderate alkalinity and a range of dissolved minerals that pose specific challenges to industrial reverse osmosis (RO) systems. While not excessively hard, the water often contains elevated silica and iron concentrations that require thoughtful system design and ongoing care to ensure longevity and performance.
Key Water Characteristics in 43339 Affecting RO System Design
Understanding the local water chemistry is critical when selecting and configuring a commercial industrial reverse osmosis system in 43339. This area's water frequently shows:
- Moderate hardness: Calcium and magnesium levels usually fall within a mid-range hardness spectrum that can contribute to membrane scaling if not managed properly.
- Noticeable silica content: Silica in feed water tends to accumulate on membranes, forming a hard-to-remove scale that reduces flow rates and recovery efficiency.
- Iron presence: Dissolved iron, often combined with manganese, can precipitate within system components, leading to fouling and increased cleaning frequency.
- Variable alkalinity: Fluctuations in pH necessitate corrosion-resistant materials and sometimes pre-treatment to stabilize feed water conditions.
Choosing the Right System Capacity and Configuration
Given these water characteristics, sizing and selecting system components for commercial or industrial operations in 43339 involves several considerations:
- Flow rate requirements: Industrial processes here typically need consistent volumes of purified water. Selecting systems with sufficient membrane surface area ensures steady output without overloading individual membranes.
- Pre-treatment needs: To mitigate silica and iron challenges, incorporating multimedia filtration, water softening, or oxidation filters before the RO membranes is common practice.
- Recovery rate optimization: Target recovery rates should balance water conservation with fouling risk. In 43339, aiming for moderate recovery (~75%) helps limit scaling while maximizing water savings.
- Modular design: For businesses anticipating growth or fluctuating demand, modular RO systems allow capacity adjustments without full system replacement.
Installation Considerations Specific to 43339 Industrial Sites
Installing an industrial reverse osmosis system in 43339 requires attention to both site conditions and local water supply variables:
- Space allocation: Facilities often have limited indoor room; compact skid-mounted systems or customizable layouts help integrate RO units efficiently.
- Feed water variability: Although generally stable, seasonal changes or nearby agricultural activities can impact feed water quality. Installing real-time monitoring equipment can alert operators to shifts that necessitate system adjustment.
- Wastewater management: RO systems generate a brine concentrate that must be handled according to local regulations. Planning for adequate discharge or recycling systems is essential to avoid compliance issues.
- Power supply compatibility: Ensuring reliable and appropriately rated electrical supply is crucial, as power interruptions can damage control panels or membranes.
Maintenance Protocols Tailored for Local Conditions
Proper maintenance ensures that industrial reverse osmosis systems in 43339 operate efficiently and maintain water quality standards over time. Recommended maintenance practices include:
- Regular membrane cleaning: Due to silica and iron accumulation tendencies, membranes often require scheduled chemical cleanings every 3 to 6 months, depending on system loading and feed water quality fluctuations.
- Pre-filter replacement: Sediment and carbon pre-filters should be checked and changed routinely to prevent particulate buildup and protect membranes from chlorine-related degradation.
- System monitoring: Pressure differentials across membranes, permeate flow rates, and rejection rates are key indicators of system performance and should be recorded to identify developing issues early.
- Valve and pump inspection: Mechanical components exposed to variable water chemistry can experience wear or fouling; regular lubrication and visual checks extend equipment life.
Long-Term Considerations For Industrial RO Operations in 43339
Businesses investing in commercial industrial reverse osmosis systems in this region can expect a technology well adapted to their needs if systems are properly selected and maintained. Some long-term factors to keep in mind include:
- Membrane lifespan: Typically ranging from 3 to 5 years under optimal conditions, membranes in 43339 may experience accelerated wear if pre-treatment is inadequate or maintenance intervals are missed.
- Water quality trends: Monitoring local water supply changes such as increased industrial discharge or agricultural runoff can inform adjustments needed in treatment strategies.
- Energy efficiency: Advances in pump and system design can improve energy consumption over time; evaluating upgrades during scheduled maintenance can reduce operational costs.
- Scalability: As water demand grows, integrating additional membrane modules or parallel systems can provide increased capacity without downtime.
Summary
For commercial and industrial water treatment in the 43339 area, reverse osmosis remains a reliable method to address locally prevalent water concerns such as moderate hardness, silica, and iron content. Selecting appropriately sized systems with tailored pre-treatment, combined with diligent maintenance practices sensitive to local water chemistry, ensures optimal system performance and longevity. Planning installation carefully to accommodate site-specific factors and anticipating future capacity needs will safeguard your water treatment investment and maintain consistent water quality for your operations.
Advanced Pre-Treatment Techniques for Enhanced RO Performance
Beyond standard filtration and chemical conditioning, advanced pre-treatment methods can significantly improve reverse osmosis system efficiency and membrane longevity. These techniques target specific contaminants and help to mitigate common fouling mechanisms experienced in the 43339 region.
Electrodeionization (EDI)
Electrodeionization combines ion exchange resins and electricity to continuously remove ionized species from water without the need for chemical regenerants. Incorporating EDI as a final polishing step after traditional RO can produce ultrapure water for processes requiring stringent water quality standards.
Ultrafiltration (UF) Systems
Ultrafiltration membranes provide a physical barrier to suspended solids, colloidal particles, bacteria, and some viruses. Installing UF prior to the RO system reduces particulate load and biofouling potential, leading to more stable flux rates and reduced chemical cleaning frequency.
Advanced Oxidation Processes (AOP)
AOPs such as ozonation or UV combined with hydrogen peroxide can degrade organic compounds and trace contaminants that contribute to membrane fouling. In regions where agricultural runoff or industrial discharges elevate organic load, AOPs act as an effective pretreatment step.
Automation and Control Strategies to Optimize RO Systems
Incorporating automation into industrial reverse osmosis systems enhances operational reliability and simplifies maintenance. Automated control systems can dynamically adjust operating parameters in response to fluctuating feed water quality and demand.
Real-Time Water Quality Monitoring
- Installation of inline sensors for conductivity, turbidity, pH, and pressure enables continuous assessment of feed and permeate water quality.
- Data from these sensors allows for early detection of membrane fouling, scaling, or feed water variability, facilitating proactive maintenance.
Variable Frequency Drives (VFDs)
- Using VFDs on feed pumps and booster pumps enables fine control of feed pressure and flow rate, optimizing energy consumption based on system demand.
- VFDs contribute to smoother system startups and shutdowns, reducing stress on mechanical components and membranes.
Automated Chemical Dosing
- Automated dosing pumps ensure precise and consistent addition of antiscalants, pH adjusters, and biocides.
- Feedback loops can adjust dosing rates based on real-time water chemistry data, minimizing chemical waste and preventing overdosing.
Environmental Compliance and Waste Management
Industrial reverse osmosis operations must consider environmental regulations, particularly concerning concentrate (brine) disposal and chemical usage. Proper management mitigates ecological impact and ensures regulatory compliance.
Brine Concentrate Handling
- Discharge options include municipal sewer systems (subject to permit requirements), evaporation ponds, deep well injection, or zero liquid discharge (ZLD) systems.
- Brine characterization is essential to determine the most suitable disposal method, accounting for salinity, heavy metals, organics, and other constituents.
- Precipitation or crystallization units can reduce volume and recover valuable salts or minerals from concentrate.
Chemical Storage and Disposal
- Proper containment and handling protocols for chemicals like antiscalants, cleaning agents, and pH adjusters prevent accidental releases.
- Spent chemical solutions and cleaning wastes must be neutralized or treated before disposal in accordance with local regulations.
- Maintaining Material Safety Data Sheets (MSDS) and training personnel on safe chemical practices promotes workplace safety.
Emerging Technologies Impacting Industrial RO
Ongoing research and innovation continue to expand the capabilities and cost-effectiveness of reverse osmosis technologies relevant to industrial users in the 43339 area and beyond.
Graphene-Based Membranes
Membranes incorporating graphene materials show promise for increased permeability and contaminant rejection, potentially allowing higher throughput at lower pressure and energy requirements.
Membrane Surface Modifications
- Coatings that impart anti-fouling or antibacterial properties reduce biofilm formation and scaling.
- These modifications extend membrane lifespan and reduce cleaning frequency.
Integration with Renewable Energy Sources
- Pairing RO systems with solar or wind power supports sustainable water treatment operations, especially in off-grid or remote industrial sites.
- Energy storage technologies enable continuous system operation despite intermittent renewable energy availability.
Customized Solutions for Specific Industrial Sectors
Each industrial sector may face unique water treatment challenges, requiring tailored RO system configurations and supplementary processes.
Food and Beverage Industry
- Emphasis on hygienic design to prevent microbial contamination.
- Use of food-grade materials and compliance with sanitary standards.
- Enhanced pre-treatment to remove organics and suspended solids that impact taste and safety.
Chemical Manufacturing
- Treatment of high TDS and scaling ion concentrations necessitates robust anti-fouling measures.
- Occasionally, higher temperature feeds require thermally stable membrane materials.
Power Generation
- High purity water is critical for boiler feedwater to prevent scaling and corrosion.
- Integration with demineralization and condensate polishing units for comprehensive water quality control.
Training and Operator Skill Development
Effective RO system operation depends on knowledgeable personnel who understand system intricacies and maintenance requirements.
Regular Training Programs
- Provide operators with instruction on system components, troubleshooting, and safety protocols.
- Update staff on emerging technologies and industry best practices.
Access to Technical Support
- Establish relationships with equipment manufacturers and water treatment consultants for expert guidance.
- Utilize remote monitoring tools to allow offsite experts to assist with system diagnostics.
Conclusion: Positioning Your Industrial RO System for Future Success
By incorporating advanced pre-treatment, automation, environmental compliance measures, and sector-specific customizations, businesses in the 43339 region can maximize the benefits of their reverse osmosis water treatment systems. Continual operator training and engagement with emerging technologies will further ensure the system’s resilience and cost-effectiveness amid evolving water quality and regulatory landscapes.
Related
- Commercial Industrial Reverse Osmosis Usa Made 30217
- Commercial Industrial Reverse Osmosis Usa Made 32358
- Commercial Industrial Reverse Osmosis Usa Made 32506
- Commercial Industrial Reverse Osmosis Usa Made 33570
- Commercial Industrial Reverse Osmosis Usa Made 33920
- Commercial Industrial Reverse Osmosis Usa Made 35031
- Commercial Industrial Reverse Osmosis Usa Made 35055